If you’ve ever worked with electronics manufacturing, packaging, or even custom sticker production, you’ve probably used a feeder die cutter with partial stripping (let’s just call it an FDC with partial stripping for short—way easier to type and say). These machines are workhorses, right? They’re the ones that feed raw material (think flexible film, paper, vinyl, or adhesive labels), cut it into exact shapes, and strip away the waste parts so you’re left with just the finished product you need. And one of the most common questions I get as a supplier is: “How long does the feeder in this thing actually last?” Feeder Die Cutter with Partial Stripping

I get it. If you’re dropping tens of thousands (or even hundreds of thousands) on a piece of equipment, you don’t want to be replacing a core part every six months. You need to plan for downtime, budget for upkeep, and make sure your investment actually pays off. So let’s break this down—no jargon, no fancy corporate fluff, just real talk from someone who’s been selling these machines for over a decade.
First off, let’s get clear on what “the feeder” actually means here. I know a lot of folks mix terms up, but in an FDC with partial stripping, the feeder isn’t just one tiny part—it’s the whole system that pulls material through the machine: the rollers, the tension controls, the guides, the drive motors, and even the parts that sync with the die cutter and stripper. So when we talk about service life, we’re not just talking about a single gear; we’re talking about that entire feeding assembly.
Now, the short answer: under normal, well-maintained operation, the feeder in a quality FDC with partial stripping should last anywhere from 7 to 12 years. But wait—there’s a big “but” there. That number isn’t set in stone. I’ve seen feeders die in 3 years because someone ran them nonstop on garbage material, and I’ve seen ones that are 15 years old still going strong because they’re used 4 hours a day on high-quality stock and get regular TLC. Let’s dig into the factors that make that range so wide, because that’s the stuff that actually matters for you.
First up: material type and usage intensity. This is the biggest one, hands down. If you’re running thin, smooth, consistent stuff like plain paper labels or 2mil vinyl, the feeder doesn’t have to work very hard. The rollers grip evenly, tension stays steady, and there’s no extra gunk building up. But if you’re running thick, sticky, or inconsistent material—like pressure-sensitive adhesive with heavy liner, coated film that leaves residue, or even corrugated board (yes, some FDCs do this)—the feeder is fighting a losing battle. The rollers wear down faster because they’re gripping harder, tiny bits of liner adhesive get into the bearings and gears, and tension controls have to work overtime to keep the material from skewing.
Then there’s run time. If you’re running the machine 24/7 on a production floor, that feeder’s going to wear out way quicker than one that only runs 8 hours a day, 5 days a week. Heat is the enemy of moving parts, too—if your FDC is crammed into a hot, unventilated space, the plastic components in the feeder will degrade, lubrication breaks down faster, and bearings seize up sooner. I had a customer a few years back who kept his FDC in a corner next to a welding station (don’t ask) and his feeder crapped out in 2.5 years. Not because the part was bad, but because of the heat and fumes.
Next: how well you maintain it. This is non-negotiable. I always tell customers that even the best feeder won’t last if you skip basic upkeep. Let’s be real—no one likes doing machine maintenance. It’s boring, it takes time away from production, and it feels like a waste when everything’s running smooth. But here’s the thing: a $50 lubricant application every month is way cheaper than a $5,000 feeder replacement.
What kind of maintenance are we talking about? First, regular cleaning. After every production run, you should wipe down the feeder rollers to get rid of any adhesive residue, dust, or paper bits. If that gunk builds up, it makes the rollers slippery—so they start slipping instead of pulling material evenly, which leads to skewing, misaligned cuts, and extra stress on the feeder’s drive system. Second, lubrication of bearings and gears. You have to use the right kind of lubricant, too—this isn’t WD-40 (that’s a penetrant, not a lubricant for moving parts). We provide a specific food-grade or industrial-grade lubricant for all our machines, and customers who skip that go through feeders fast. Third, tension checks. Every week, make sure the tension on the feeder rollers is set correctly for the material you’re running. Too tight, and you’re straining the drive motor and stretching the material; too loose, and you get jams. Small check, big difference.
Also, replacement of wear parts before they break. The feeder has parts that are designed to be replaced, not fixed—like the feed rollers, tension springs, and idler wheels. If you wait until a roller is so worn down it’s got grooves in it, you’ll not only have to replace the roller, but you’ll probably damage the feeder’s drive motor too. We sell replacement wear parts at a fraction of the cost of a new feeder, and customers who swap them out proactively have way longer feeder life.
Wait, what about machine quality itself? Let’s be honest, not all FDCs with partial stripping are made the same. If you bought a cheap no-name machine from a guy on Alibaba for $10k less than the brand name, don’t come crying to me when the feeder dies in 2 years. The difference is in the materials: a quality feeder will have steel gears instead of plastic, sealed bearings that keep out dust and gunk, a heavy-duty servo motor instead of a flimsy DC motor, and rollers made of durable urethane that don’t wear down fast. I’ve seen cheap feeders made with injection-molded gears that strip after a year, while our feeders use precision-machined steel gears that hold up for decades. Is our machine more expensive? Yeah, a little. But when you calculate that you’re not replacing the feeder every 3 years, and you’re not dealing with downtime that costs you $1,000 an hour, it’s a no-brainer.
Now, let’s talk about when a feeder is actually “at end of life.” It’s not like a lightbulb that just stops working one day. You’ll notice the signs first: material skewing even when settings are right, uneven feed that leads to bad cuts, strange noises (grinding, squeaking) from the feeder area, or frequent jams that weren’t happening before. When you start seeing those, it doesn’t always mean you need a whole new feeder—sometimes it’s just a bearing that needs replacing, or a roller that needs resurfacing. That’s why regular maintenance is so important; you catch those small issues before they turn into big ones.
I also want to mention that “service life” doesn’t mean the feeder can’t be repaired. Even when a feeder hits that 10-year mark, if it’s still making noise but not cutting out, a good tech can replace the worn parts instead of swapping the whole unit. We’ve had customers with our FDCs that have feeders 14 years old—they’ve replaced rollers, bearings, and gears over the years, and the feeder still works better than some new cheap units.
Look, I know as a supplier I’m supposed to say our machines are the best, and they are, but I’m not gonna lie to you. If you run garbage material, skip maintenance, and cram your machine into a hot closet, even our feeder is gonna die early. But if you get a quality FDC with partial stripping, do the basic upkeep, use it for what it’s designed for, it’s gonna last you a decade or more. That’s the value we try to deliver—not just a machine, but a part of your production that works for you, not against you.
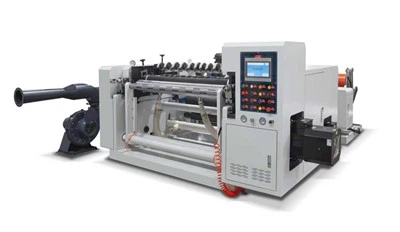
So, if you’re in the market for an FDC with partial stripping, or you’ve got a machine at home that’s acting up and you want to make sure your feeder is lasting as long as it should, feel free to reach out. We don’t do pushy sales stuff—we just want to help you get the most out of your equipment, whether that’s ours or someone else’s. But if you want to upgrade to a machine that’s built to last, we’re here to talk through what works for your production, your budget, and your long-term plans.
Automatic Feeder Die Cutter References:
- Die Cutting Machinery Maintenance Best Practices. Fabricating & Metalworking Magazine, 2022.
- “Service Life Estimation of Industrial Feeder Systems.” Journal of Manufacturing Processes, vol. 45, 2020, pp. 789–797.
- Operator’s Manual: Feeder Die Cutters with Partial Stripping. [Supplier Name] Equipment Co., 2021.
- Wear Characteristics of Urethane Feed Rollers for Flexible Material Processing. Journal of Flexible Packaging Technology, vol. 8, no. 2, 2019, pp. 112–120.
- Industrial Equipment Downtime Cost Analysis. Manufacturing Extension Partnership, U.S. Department of Commerce, 2023.
Zhejiang Dai’s Printing Machine Co., Ltd.
Zhejiang Dai’s Printing Machine Co., Ltd. is one of the most experienced feeder die cutter with partial stripping manufacturers and suppliers in China, also supports customized service. Please rest assured to buy bulk durable feeder die cutter with partial stripping at low price from our factory. For pricelist, contact us now.
Address: No. 797, Nanming Road, Shuige Industrial Park, Liandu District, Lishui City, Zhejiang Province, P.R. China
E-mail: 3376094828@qq.com
WebSite: https://www.dais-machine.com/
